
 en
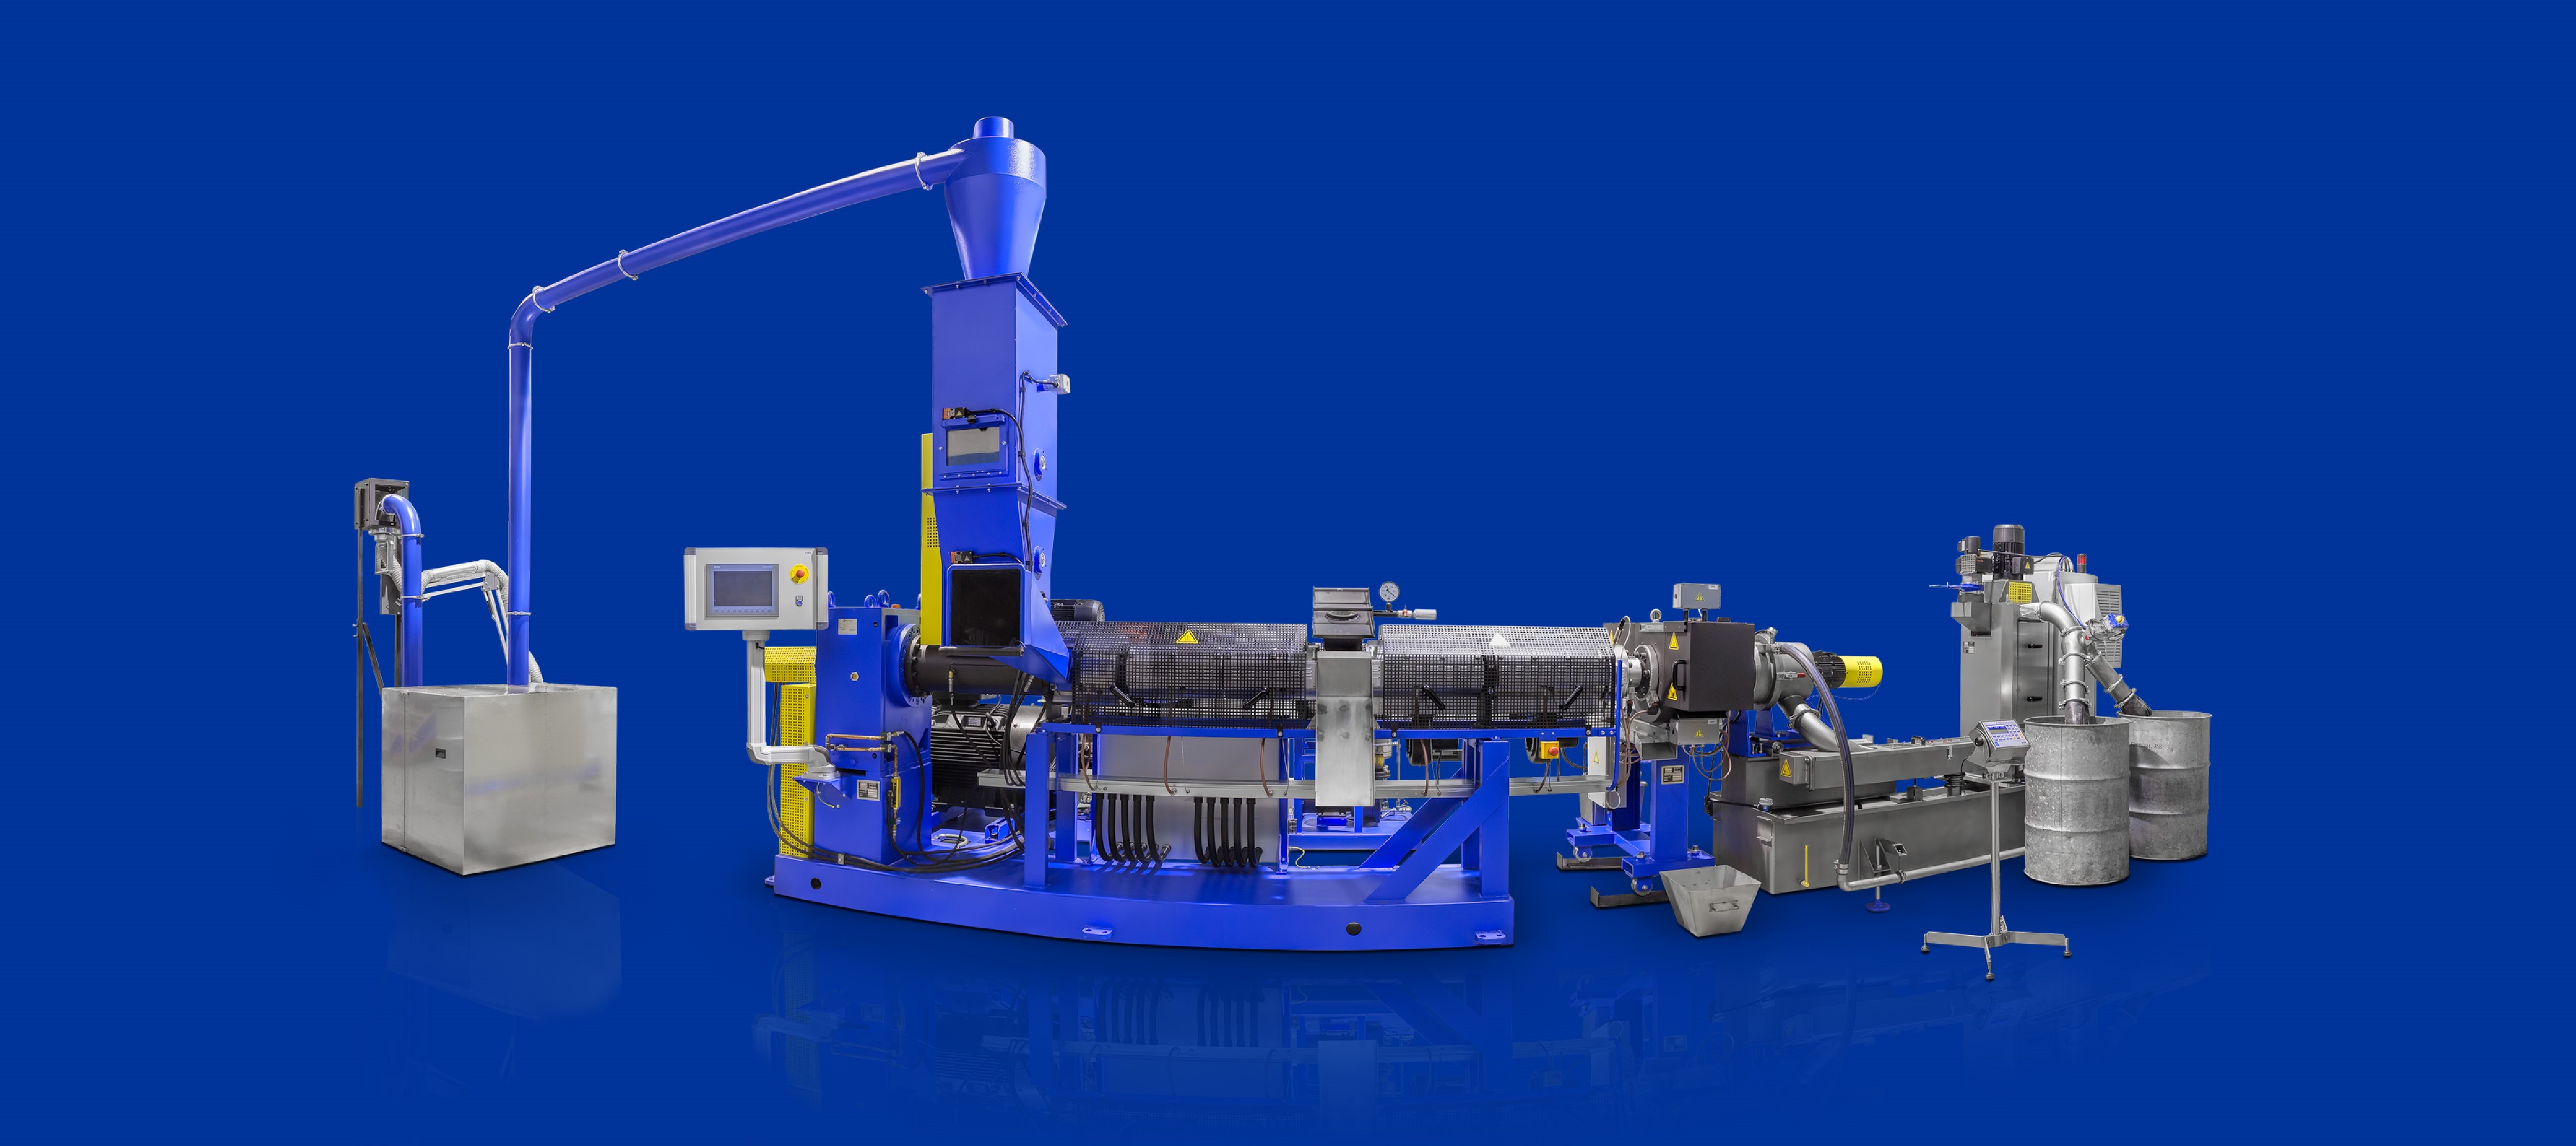
Offline Extruder for Plastic Recycling: Conical Single Screw by SIKOPLAST
Anyone looking to process thermoplastic production waste into regranulate requires an extruder capable of reliably handling a wide range of materials, regardless of bulk density, residual moisture, or surface treatment. Standard extruders with cylindrical screws quickly reach their limits when processing lightweight, non-free-flowing materials.
The SIKOPLAST Offline Extruder operates with a conical single screw specifically developed for these requirements. It processes thermoplastics into high-quality regranulate with throughput capacities ranging from 30 kg/h to over 1,300 kg/h.
Conical Single Screw: Why Screw Geometry Determines Pellet Quality
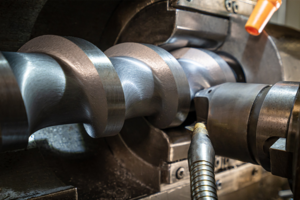
The key difference compared to standard systems lies in the feeding zone. The conical geometry of the SIKOPLAST screw generates the pressure required for lightweight and bulky materials — without the need for upstream agglomerators or cutter compactors.
What This Means for the Process
- The material is not exposed to thermal pre-stressing before the actual melting process
- No oxidative pre-stressing caused by agglomerators: the first heat input occurs only inside the extruder itself
- Melting takes place in an oxygen-free environment, preventing material degradation caused by air contact
- The combination of heating and cooling zones allows rheologically optimized melt temperature profiles
- The screw geometry can be adapted to the specific material when required
- Since the feed zone is wider than the discharge zone, the extruder can efficiently feed loose and bulky materials in large quantities
The result is homogeneous regranulate with stable quality, ready for direct use in downstream production processes.
Material Range: What the Offline Extruder Can Process
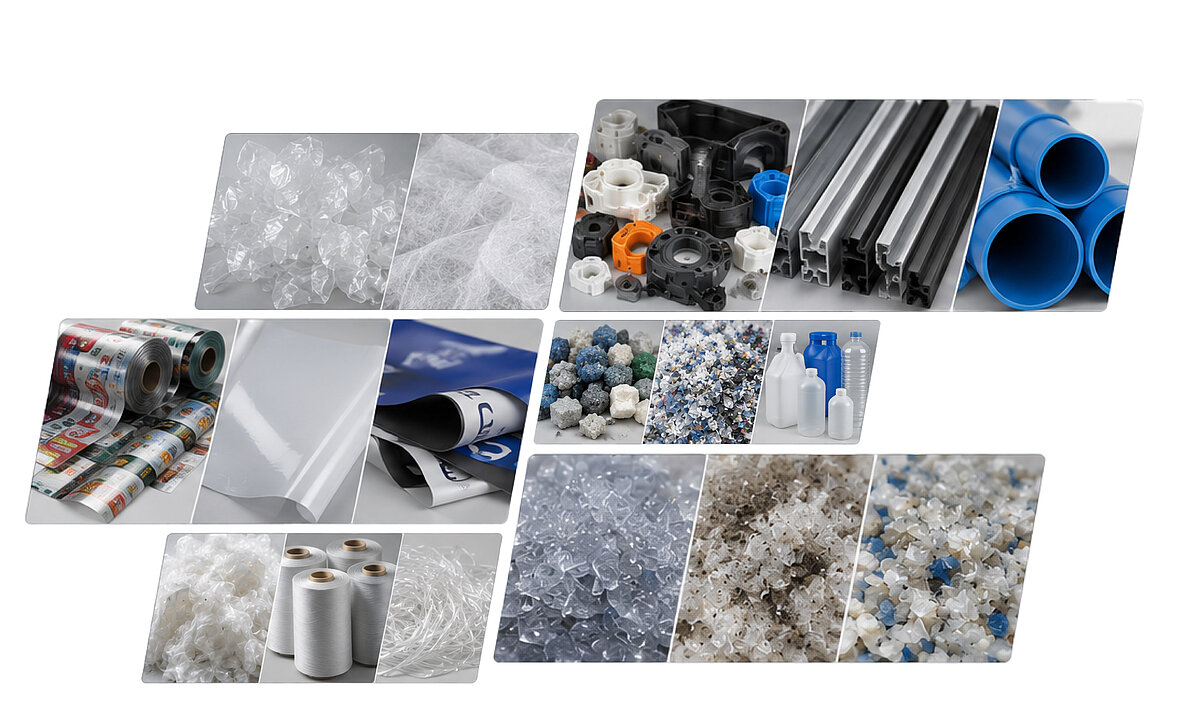
The Offline Extruder is designed for all thermoplastic materials. The material range includes:
- Films and nonwovens
- Injection-molded parts, profiles, and pipes
- Start-up lumps, regrind, and hollow bodies
- Fibers, yarns, and monofilaments
- Printed and coated materials
- Slightly moist and slightly contaminated materials (up to approx. 2% residual moisture)
For critical materials — such as moist or printed materials — the extruder can be equipped with a degassing zone and vacuum pump. Volatile substances are extracted from the melt before they can affect pellet quality.
Buffer Silo and Discontinuous Feeding: Constant Throughput With Minimal Labor
The Offline Extruder is equipped as standard with a buffer silo mounted directly onto the feeding section. The silo stabilizes material flow and ensures uniform feeding of the extruder regardless of the input material.
The buffer silo can be fed discontinuously, reducing labor requirements in the feeding area. A distinction must be made between unshredded and pre-shredded material:
Unshredded Material
This material must first be pre-ground using a granulator. Four feeding options are available for supplying the granulator:
- Manual feeding by the machine operator
- Conveyor belt feeding
- Pneumatic conveying
- Fully automatic roll feeding
Pre-Shredded Material
Already shredded materials can be conveyed pneumatically directly into the extruder buffer silo without requiring a granulator. On request, dosing stations for additives and masterbatches can also be integrated.
Technical Data
| Feature | Value |
|---|---|
Throughput | 30–1,300+ kg/h |
Material Range | All thermoplastics |
Screw Geometry | Conical single screw, customizable |
Feeding | Manual, conveyor belt, pneumatic, roll feeding |
Optional Equipment | Degassing zone and vacuum pump (for critical materials) |
Output | Regranulate |
Buffer Silo | Standard, mounted directly on feed section |
Integration Into the SIKOPLAST Offline Extrusion Line
The Offline Extruder is a core component of the SIKOPLAST offline extrusion line. As part of a complete system, it can be expanded with a granulator, screen changer, pelletizing system, and bagging station to create a complete regranulation line.
FAQ
Why does the SIKOPLAST Offline Extruder not require an agglomerator?
The conical screw geometry generates the compaction pressure required for lightweight and non-free-flowing materials directly in the feeding zone. As a result, upstream agglomerators or cutter compactors are unnecessary because the screw itself performs this function completely.
Can printed or coated materials be processed?
Yes. Printed and coated materials can be processed directly. For materials with high moisture content or heavy printing, SIKOPLAST recommends a configuration with a degassing zone and vacuum pump.
What throughput capacities are possible?
Standard systems cover capacities from 30 kg/h to over 1,300 kg/h. The exact configuration depends on the material, bulk density, and contamination level.
Is retrofitting with a melt filtration system possible?
Yes. Screen changers can be connected to the extruder via adapter flanges. They improve material purity and can be adapted flexibly to different contamination levels.
What information is required for a quotation?
Material type and form, desired throughput capacity, contamination level, residual moisture content, and information about the available installation space.